Choosing the best telecentric macro lens for metrology is not a simple specification exercise. It is a measurement decision.
MarketsandMarkets estimates that the global machine vision market will grow from about USD 11.7 billion in 2023 to USD 20.6 billion by 2028. Its report identifies inspection accuracy, automation, and dimensional consistency as major growth drivers. These pressures make lens selection increasingly important. A small error at the imaging stage can become a rejected batch, especially when inspecting connectors, molded parts, or machined edges.
A telecentric macro lens reduces perspective distortion and keeps magnification more stable across depth. Imagine measuring a 10 mm metal pin. With a conventional lens, the near edge may appear slightly larger than the far edge. With a telecentric design, that visual shift is greatly reduced. It is not magic.
John Greivenkamp, an optical metrology educator and author of Principles of Optics, offers a useful measurement reminder: “A measurement is only as good as its uncertainty budget.” This principle applies directly to telecentric imaging. Resolution alone cannot guarantee dependable results. Working distance, sensor size, aperture, depth of field, distortion, illumination, and calibration must work together.
Edmund Optics technical guidance also emphasizes that telecentric systems are valuable when object size must remain consistent despite position changes. However, the “best” lens depends on the application. A lens with excellent distortion control may provide less light. A compact model may limit working distance. Even experienced engineers can overlook lighting geometry.
The following comparison examines these trade-offs, using published industry data and practical metrology criteria. It also questions where telecentric macro lenses genuinely improve accuracy—and where they simply increase system cost.
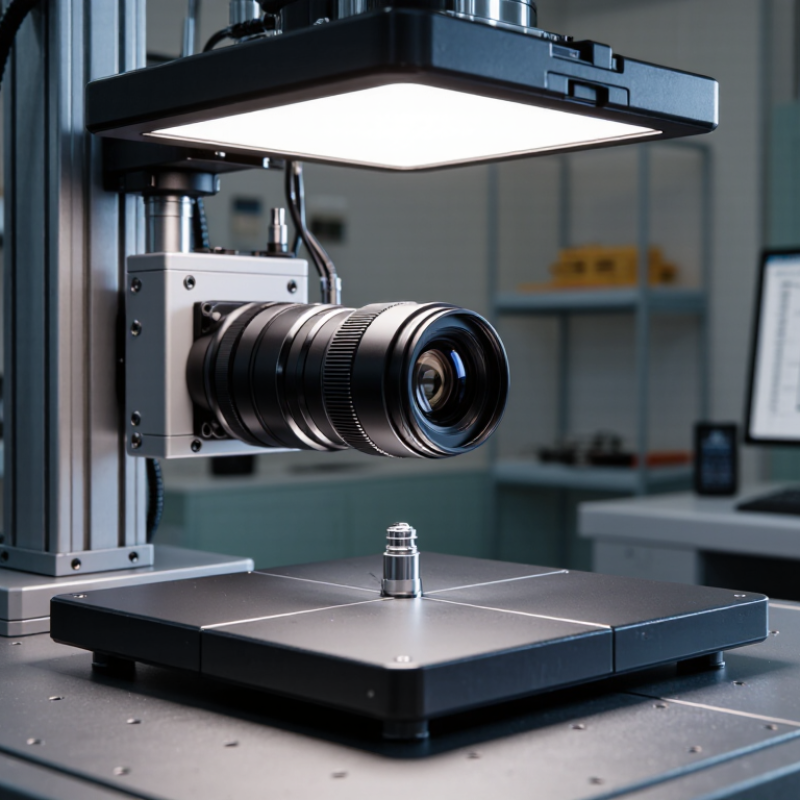
A telecentric macro lens is designed to keep magnification nearly constant across object depth. Its entrance pupil sits optically at infinity. Therefore, chief rays travel almost parallel to the optical axis. A 2 mm pin may look like 2 mm, even when its front and rear edges sit at different distances. This sharply reduces perspective error and edge-position shifts. Standard macro lenses cannot provide this stability. They often make nearer features appear larger.
For metrology, the best telecentric lens depends on field of view, sensor size, working distance, and allowable distortion. ISO 10360-7 emphasizes controlled acceptance and reverification tests for imaging-based coordinate measurement systems. That matters because a visually sharp image can still produce inaccurate dimensions. The 2024 MarketsandMarkets machine vision report valued the global machine vision market at about USD 13.7 billion and projects approximately USD 20.6 billion by 2029. Growing inspection demand makes repeatable optics more important. Yet the lens alone cannot correct poor lighting, vibration, or calibration mistakes.
Tips: Measure the largest part first. Choose a lens with enough field coverage. Leave space for illumination. Check distortion across the entire image, not only at the center. Use a calibrated target at several depths. Small errors become visible. Also, telecentric lenses are not magic; limited depth of field and higher cost can complicate a practical setup. I have seen operators trust a crisp image too quickly. That is a useful warning.
Telecentricity keeps image magnification nearly constant when the object moves slightly along the optical axis. This matters during dimensional inspection. A conventional lens may make a hole appear larger when it sits closer to the camera. The same hole may appear smaller when positioned farther away. That shift can create measurement errors, even when the part remains within its fixture.
A telecentric macro lens reduces this perspective effect by using carefully controlled chief rays. Edges remain more stable across the field of view. For example, a machined pin can keep nearly the same measured diameter despite small height variations. In production, this supports repeatable checks of gaps, slots, holes, and molded edges. The benefit becomes clearer when parts have uneven surfaces or imperfect fixturing.
However, telecentricity does not solve every metrology problem. Lighting, sensor resolution, focus, calibration, and thermal changes still influence results. I once treated lens selection as the main accuracy decision, but inconsistent backlighting caused larger errors than expected. A reliable setup needs controlled illumination and a calibrated reference artifact. Working distance also deserves attention. A lens may offer excellent telecentric performance but provide too little room for the fixture or lighting hardware. Careful testing with real parts is essential, because glossy surfaces, burrs, and soft edges can challenge even a technically strong optical system.
The best telecentric macro lens is not defined by magnification alone. Optical specifications must match the measurement task, camera, lighting, and part geometry. Object-space telecentricity keeps apparent size stable when the component moves slightly along the optical axis. This reduces dimensional errors at the image edge. Check the stated telecentric angle, not only the marketing description.
Magnification determines field of view and pixel resolution. Working distance matters when fixtures, lighting, or tall parts surround the target. Numerical aperture influences resolution and depth of field. Higher resolution can reveal small defects, but it may reduce usable focus depth.
Distortion should remain very low across the complete sensor area. Also verify image-circle coverage, especially with larger sensors. MTF data at the required magnification is more useful than a single center-resolution figure. In practice, I compare calibrated images of a reference artifact, because specifications do not always predict real bench performance perfectly.
Tips: Match the lens magnification to the smallest feature, then confirm the full part fits the field of view. Check illumination compatibility before purchase. Coaxial light can expose flat surface marks, while directional light may reveal height changes. Keep the working distance physically realistic. I have occasionally chosen excessive magnification and lost useful context. That was a preventable mistake. Consider wavelength transmission, camera pixel size, mounting stability, and temperature drift. A lens may perform well in a catalog test, yet require careful calibration in your measurement environment.
Telecentric macro lenses differ less by advertised magnification than by measurement behavior. In practical metrology, I compare edge fidelity, distortion, working distance, and illumination compatibility. A 0.5x lens may inspect a stamped hole clearly, yet fail when the part shifts several millimeters off-axis. That matters on a busy production fixture.
High-performing designs keep magnification nearly constant as object distance changes. This reduces apparent size errors at the part’s edges. Their long working distance leaves room for ring lights, clamps, and protective windows. However, longer distance can reduce available light. Aperture settings then become critical. Stopping down may increase depth of field, but diffraction can soften tiny features.
Fixed-magnification lenses often provide simpler calibration and stable image geometry. Variable-magnification systems offer flexibility across different parts, although calibration takes longer. Sensor coverage must match the camera, not just the advertised image circle. Check it with a certified grid target. No lens wins every test. I have seen a sharp optic underperform because its illumination angle exposed scratches as false edges. I also prefer checking repeatability across temperature changes, because laboratory sharpness does not guarantee factory consistency.
The comparison below summarizes typical published performance ranges for industrial telecentric macro-lens configurations. Exact specifications vary by optical design, magnification, sensor coverage, aperture, and illumination setup.
| Evaluation Criterion | Low-Magnification Configuration 0.1×–0.3× | General-Purpose Configuration 0.3×–0.5× | Precision Metrology Configuration 0.5×–1.0× | High-Magnification Configuration 1.0×–2.0× |
|---|---|---|---|---|
| Primary Use | Large-part inspection, dimensional screening, and presence/absence checks | Component inspection, connector measurement, and assembly verification | High-accuracy dimensional measurement and profile inspection | Small-feature measurement, micro-components, and fine surface inspection |
| Typical Working Distance | 100–200 mm | 80–120 mm | 60–110 mm | 40–80 mm |
| Object-Side Telecentricity | Typically below 0.2° | Typically below 0.15° | Typically below 0.1° | Typically below 0.1° |
| Perspective Error | Low; generally suitable for routine dimensional inspection | Very low; suitable for repeatable edge and hole measurements | Extremely low; preferred when part height variation must not change apparent size | Extremely low, but alignment and focusing become more critical |
| Typical Distortion | Approximately <0.1% to 0.3% | Approximately <0.1% to 0.2% | Approximately <0.05% to 0.1% | Approximately <0.05% to 0.1% |
| Typical Depth of Field | Relatively high; often preferred for uneven or large parts | Moderate to high, depending on numerical aperture and f-number | Moderate; stopping down can improve depth of field at the expense of light | Limited; precise Z-axis control is commonly required |
| Recommended Sensor Coverage | Medium to large sensors, selected according to the required field of view | Commonly compatible with 1-inch to APS-C-class sensors | Often optimized for 1-inch, APS-C, or similar machine-vision sensors | Usually selected for smaller fields of view and high pixel sampling |
| Field of View at a 12 mm Sensor Width | Approximately 40–120 mm, depending on magnification | Approximately 24–40 mm | Approximately 12–24 mm | Approximately 6–12 mm |
| Image-Space Telecentricity | May be non-telecentric or partially telecentric | Often near-telecentric in industrial designs | Frequently telecentric or near-telecentric for stable sensor illumination | Design-dependent; verify compatibility with the camera and illumination system |
| Optical Resolution | Typically adequate for coarse edges and large features | Suitable for general machine-vision measurement | Designed for high-contrast edges and repeatable sub-pixel measurement | High feature sampling, but performance depends strongly on diffraction, focus, and sensor pixel size |
| Illumination Compatibility | Coaxial, ring, and diffuse front lighting are commonly used | Ring, bar, dome, and telecentric backlighting are commonly used | Telecentric backlighting, coaxial lighting, and controlled diffuse illumination are preferred | Coaxial, dark-field, and specialized narrow-angle lighting may be required |
| Measurement Repeatability | Good when part position and height are controlled | Very good for routine dimensional inspection | Excellent when calibrated with stable mechanics and controlled lighting | Excellent for small features, provided focus and vibration are tightly controlled |
| Typical Trade-Off | Large field of view but lower pixel-level detail | Balanced field of view, working distance, and measurement performance | Best balance for precision metrology, with higher cost and tighter setup requirements | High detail but smaller field of view, reduced depth of field, and greater sensitivity to alignment |
| Best Choice When | The part is large, depth variation is significant, and measurement tolerance is moderate | A single lens must handle a broad range of common inspection tasks | Dimensional accuracy, low perspective error, and repeatability are the primary priorities | Features are very small and the inspection system can provide accurate focus and positioning |
For metrology applications, the best lens is normally selected by matching magnification, field of view, working distance, sensor size, distortion, telecentricity, and illumination—not by magnification alone.
Choosing the best telecentric macro lens starts with the measurement, not the camera. Define the smallest feature, tolerance, surface finish, and inspection distance. A lens with suitable magnification should fill the sensor without cropping important edges. Too much magnification wastes field of view. Too little makes defect detection uncertain. Measure the actual part, not only its drawing.
Object-space telecentricity matters when dimensional accuracy is critical. It reduces apparent size changes caused by small height differences. Check the specified telecentric error and distortion across the full image area. A part may measure correctly at the center but drift near the corners. That is easy to miss. Working distance also affects safety, lighting, and fixture design. Leave enough space for the part and illumination.
Match the lens to the sensor format, pixel size, and required resolution. Depth of field deserves a practical test. A shiny metal edge may look sharp under one light and unclear under another. Coaxial light can help with flat surfaces, while low-angle light reveals burrs and scratches. Test representative parts, including the worst samples. Calibration targets can verify repeatability, but they cannot replace production trials. A lens that performs well in a laboratory may struggle with vibration, dust, or uneven mounting. That limitation should be recorded, not ignored.
How Can You Choose the Best Lens for Your Application?
Typical engineering targets for telecentric metrology applications. Lower distortion and smaller object-space sampling support more accurate dimensional measurements. Select the lens according to field of view, working distance, sensor size, and required measurement tolerance.
